How to choose filter press fabric for industrial dewatering
Why filter press fabric selection matters
Filter press fabric is the working separation layer in a plate-and-frame, recessed-plate or membrane filter press. It is more than a replaceable textile part. The fabric influences how quickly liquid leaves the chamber, how well solids are retained, how cleanly the cake releases and how often operators must stop the press for washing or replacement.
A sound selection starts with the slurry, not with a generic fabric code. Polymer, yarn type, weave, finishing and installation style all need to match the chemical exposure, temperature, particle size, cake behavior and press design. For related textile application topics, visit the Applications section.
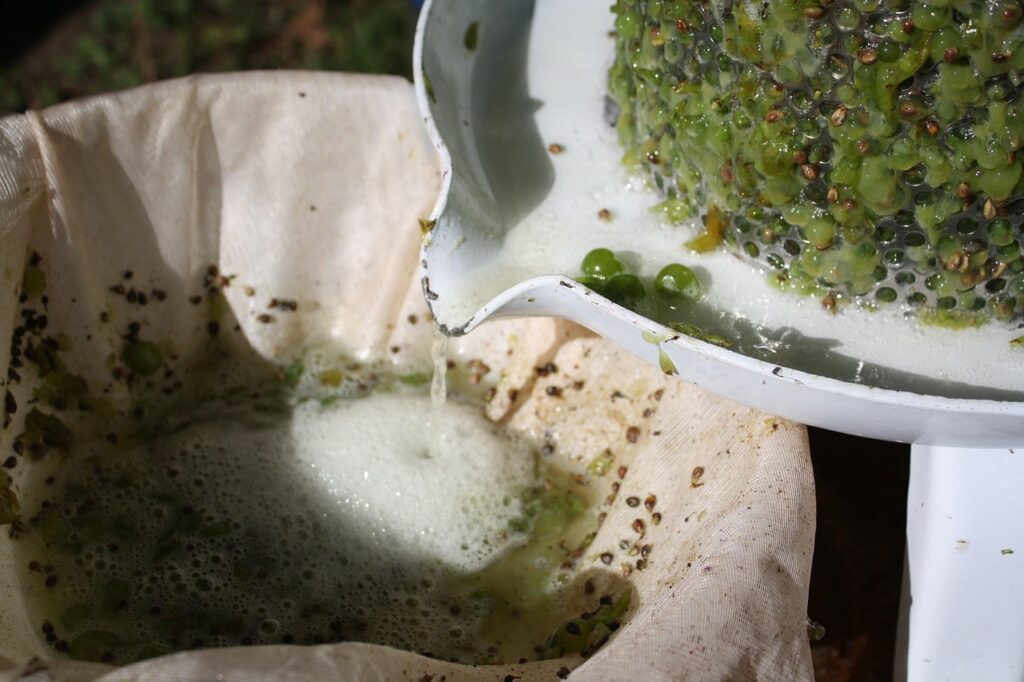
In published technical guidance on recessed-plate filter presses, the U.S. Environmental Protection Agency describes the basic operating principle clearly: solids are retained on the filter cloth while liquid passes through and drains away. That simple point explains why the cloth is so important. If the fabric is too open, fines may pass through before a stable cake forms. If it is too tight, filtration slows, pressure rises and cleaning becomes more difficult.
The practical goal is balance. Operators usually want clear filtrate, short cycles, dry cake, easy discharge and long fabric life. No single fabric maximizes all five at the same time. The right filter press fabric is the option that meets the process priorities with the fewest compromises.
Start with the slurry and process conditions
Before comparing polypropylene, polyester or nylon fabrics, define the filtration duty. Two slurries with the same solids concentration can require very different cloths if one contains coarse crystalline solids and the other contains fine, compressible or oily particles. The most useful selection data usually comes from the process itself.
- Particle size distribution: Coarse, rigid particles can often build a permeable cake on a more open fabric. Fine or colloidal particles may need a tighter weave, precoat, conditioning or a staged trial.
- Liquid chemistry: Acids, alkalis, solvents, oxidizers, oils and process additives can weaken fibers or finishes. Chemical resistance should be checked at the actual concentration and temperature, not only by polymer name.
- Temperature: Higher liquid temperature can affect fabric strength, dimensional stability, chemical attack rate and cake release behavior.
- Solids concentration: Dilute feeds may take longer to form an initial cake layer, making early-stage retention more important.
- Cake compressibility: Compressible sludge can blind fabric pores more easily than granular mineral solids, especially when pressure is increased too quickly.
- Filtrate target: A process that sends filtrate to reuse, discharge or downstream polishing may need tighter retention than a process where throughput is the main priority.
- Press configuration: Recessed plates, membrane squeeze plates, corner-feed plates, center-feed plates and gasketed designs can require different cloth shapes and attachment details.
These conditions should be recorded before ordering or changing cloth. A fabric that looks suitable in a catalogue can fail in service if it ignores the chemistry, feed conditioning or plate design.
Compare common filter press fabric materials
The fiber material sets the foundation for chemical compatibility, heat resistance, abrasion behavior and fabric cost. The table below summarizes common choices used in industrial filter press cloth discussions. It is a comparison guide, not a substitute for a compatibility check or pilot test.
| Fabric material | Typical strengths | Selection cautions |
|---|---|---|
| Polypropylene | Widely used in aqueous industrial filtration; good general chemical resistance; relatively light; often selected where cake release and cost are important. | May be unsuitable for certain oxidizing conditions, solvents or higher-temperature duties. Dimensional and thermal limits should be confirmed. |
| Polyester | Good dimensional stability and mechanical strength; often considered where temperature resistance is more demanding than standard polypropylene applications. | Strong alkali and hydrolysis conditions can be a concern, especially at elevated temperature. |
| Polyamide or nylon | Good abrasion resistance and toughness; can be useful with hard or abrasive particles when chemistry allows. | Strong acids and moisture-related dimensional changes can limit suitability in some duties. |
| PTFE, PVDF or specialty polymers | Used where chemical resistance or temperature exposure exceeds common commodity polymers. | Higher cost and availability considerations mean they are usually selected for specific severe conditions rather than general duty. |
Material selection should be conservative. For example, a fabric may resist an acid at room temperature but behave differently when the slurry is hot, abrasive and pressurized. Likewise, a polymer may survive the liquid phase but still fail early because of mechanical flexing, plate edges, chemical cleaning or poor installation.
Yarn, weave and finish decide the filtration behavior
After the polymer is chosen, construction becomes the next major decision. Two cloths made from the same polymer can behave very differently if one uses smooth monofilament yarn and the other uses multifilament or spun yarn. This is where filter press fabric selection becomes a textile engineering decision, not a simple material substitution.
Monofilament, multifilament and spun yarns
Monofilament yarn is made from single, smooth filaments. It generally supports easier cake release and easier surface cleaning because solids have fewer places to lodge. It can be a strong option where blinding, washing time and automatic cake discharge are persistent problems. The trade-off is that a very open monofilament construction may allow more fines through until a filter cake forms.
Multifilament yarn is made from many smaller filaments. It can provide more surface area and finer particle capture, which may improve early filtrate clarity in some duties. The downside is that fine solids can become trapped within the yarn bundle, making washing and long-term permeability more challenging.
Spun or staple yarn uses shorter fibers twisted together. It can offer high retention and a textile surface that captures fines, but it may also hold solids more strongly. In applications where cake release is critical, operators should test carefully before moving to a heavily retentive spun construction.
Weave and finishing choices
Plain, twill, satin and other weave structures change surface smoothness, pore geometry, strength and flexibility. Plain weaves are stable and common. Twill and satin constructions can provide smoother surfaces and different cake release behavior, but they still need to match the required retention and mechanical strength.
Finishing also matters. Heat setting can improve dimensional stability. Calendering can flatten and smooth the surface, reducing permeability while sometimes improving retention or release. Singeing may reduce loose fibers that could trap solids. Finishing should not be treated as cosmetic; it changes how liquid, solids and cleaning water interact with the fabric.
Air permeability is often used as a comparative textile property. ISO 9237:1995 describes a method for measuring the air permeability of fabrics and is applicable to industrial fabrics as well as other textile materials. For filter press work, air permeability can help compare cloth openness under controlled conditions, but it does not replace a slurry test. A real slurry contains particles, dissolved chemicals and cake structures that air testing cannot reproduce.
A practical selection matrix for filter press fabric
The following matrix gives a practical way to turn process symptoms into cloth selection questions. It does not produce an automatic answer, but it helps narrow the trial plan and avoid random cloth changes.
| Process signal | Likely fabric question | What to validate |
|---|---|---|
| Cloudy filtrate at the beginning of the cycle | Is the fabric too open for the initial cake-forming stage? | Test tighter weave, different yarn construction, improved feed conditioning or precoat strategy. |
| Long filtration cycle with low flow | Is the fabric too tight, blinded or chemically attacked? | Check permeability trend, cleaning recovery, solids conditioning and actual cloth age. |
| Cake sticks to the cloth | Is the surface too rough or the cake too adhesive? | Compare smoother monofilament, calendered finish, release treatment and discharge timing. |
| Frequent cloth blinding | Are fines entering the yarn structure or pores? | Review yarn type, weave openness, cleaning method and particle conditioning. |
| Premature tearing or edge damage | Is the issue mechanical rather than filtration-related? | Inspect plate alignment, feed pressure, wrinkles, gasket fit, plate edges and installation tension. |
| Good clarity but poor productivity | Is the retention target stricter than the process needs? | Confirm filtrate specification, then trial a slightly more open fabric or process adjustment. |
This matrix is also useful when documenting trials. Changing several variables at once makes it difficult to learn from results. Where practical, test one major variable at a time: polymer, yarn, weave, finish or operating condition. See also: Coatings.
Installation and maintenance affect cloth performance
Even a well-selected fabric can fail if it is installed poorly. Wrinkles, misaligned feed holes, damaged eyelets, poor edge sealing or uneven tension can create bypass, leakage, cake sticking and local fabric wear. In gasketed or caulked designs, the fabric must sit correctly in the sealing area. In center-feed or corner-feed plates, the feed neck and reinforcement details must match the plate geometry.
Maintenance should be based on symptoms and records, not habit alone. Useful operating indicators include cycle time, filtrate clarity, feed pressure profile, cake moisture, cake release quality, cleaning frequency and visible fabric damage. If cycle time rises but washing restores performance, blinding may be the main issue. If washing no longer restores flow, the cloth may be chemically aged, mechanically worn or permanently plugged.
Cleaning should match both the fabric and the solids. Excessive mechanical brushing can damage yarns or finishes. Aggressive chemicals can shorten fabric life if they are not compatible with the polymer. High-pressure washing can help in some plants, but if used incorrectly it may drive particles deeper into the textile or damage seams. The safer approach is to define an approved cleaning method for each slurry and fabric combination.
Replacement decisions should consider total cost, not just cloth price. A cheaper fabric that blinds quickly may increase labor, downtime, wash water, disposal volume and off-spec filtrate risk. A more expensive fabric may be justified if it reduces cycle time or improves cake discharge, but that conclusion should be based on measured operating data.
Common mistakes to avoid
Selecting by micron rating alone. Woven filter press fabrics do not behave like a simple screen. Retention depends on pore structure, yarn type, surface condition, cake formation and operating pressure. A nominal rating can be useful, but it should not be the only selection criterion.
Ignoring feed conditioning. Polymer dosing, pH adjustment, precoat use and particle agglomeration can change filtration more than the cloth itself. A fabric change may not solve a problem caused by poor conditioning.
Choosing the tightest fabric for the clearest filtrate. Very tight fabrics can reduce flow, extend cycle time and blind quickly. In many filter presses, clarity improves after the initial cake forms, so the best fabric may be the one that supports stable cake formation rather than the tightest available textile.
Copying another plant’s cloth. Similar equipment does not guarantee similar slurry behavior. Mineral shape, particle size, oils, surfactants, temperature and chemical additives can change the result.
Not inspecting the plates. Cloth damage is sometimes blamed on the fabric when the real cause is a cracked plate, sharp edge, blocked drainage surface or misaligned press.
Frequently asked questions
What is the best filter press fabric?
There is no universal best fabric. The best choice is the fabric that meets the process target for filtrate clarity, cycle time, cake release and service life under the actual slurry chemistry, temperature and pressure conditions.
Is polypropylene better than polyester for filter press cloth?
Polypropylene and polyester are both widely used, but they solve different problems. Polypropylene is often selected for broad aqueous chemical resistance and release behavior, while polyester may be considered where dimensional stability or temperature exposure points in that direction. Actual chemical compatibility should always be checked for the specific liquid and temperature.
How often should filter press fabric be replaced?
Replacement intervals vary widely by slurry, pressure, cleaning method, fabric construction and operating hours. Instead of using a fixed date only, track cycle time, filtrate clarity, washing recovery, cake release and visible wear. Replace the cloth when performance no longer returns after proper cleaning or when physical damage creates leakage or bypass.
Can one fabric handle wastewater, mining and chemical slurries?
Not reliably without validation. Wastewater sludge, mineral concentrates and chemical process slurries can differ in particle size, abrasiveness, pH, solvents, oils and temperature. The same polymer family may be used in several industries, but the construction and finish often need to be different.
Does higher air permeability always mean faster filtration?
No. Higher air permeability indicates a more open fabric under a controlled air test, but liquid filtration depends on slurry viscosity, particles, cake compressibility and blinding behavior. Air permeability is useful for comparison, while process trials show real filtration performance.